// Blog post
Maximizing Success Through Supplement Quality Control
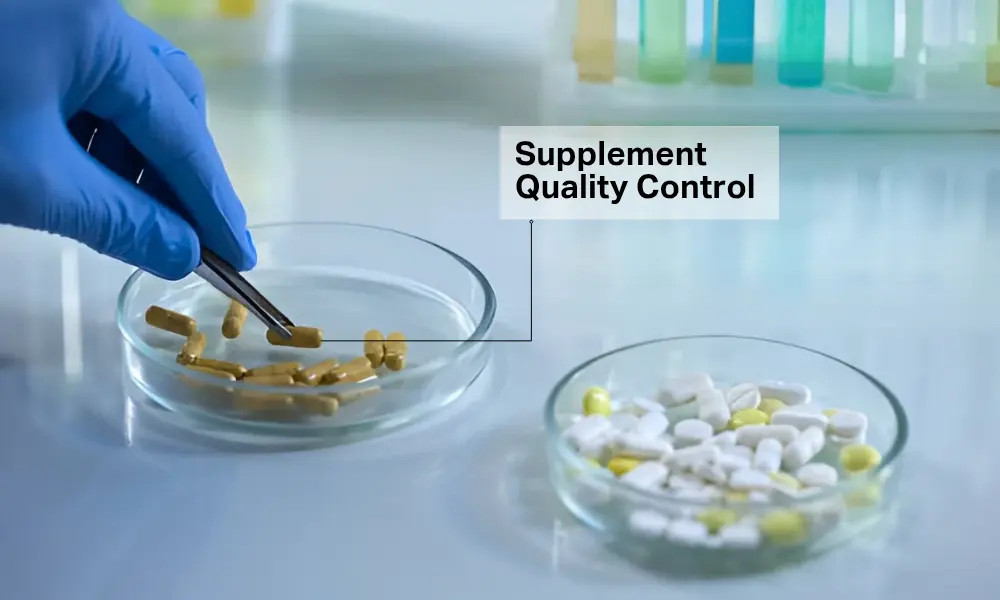
Table of Contents




Recent Posts
Popular posts
Certifications
As the nutraceutical market continues to expand rapidly, driven by heightened consumer interest in health and wellness, the importance of supplement quality control, including probiotics, cannot be overstated. This growth has intensified the demand for products that meet rigorous safety and efficacy standards. With so many supplements on the market, strict quality control is what keeps products pure, potent and compliant with safety rules. Adequate quality assurance necessitates thorough ingredient testing to identify pathogens and verify quality indicators. Additionally, supplement manufacturers in the USA must ensure traceability throughout the production process to minimize risks and maintain brand integrity. Strong quality control protects customers and builds the trust a brand needs to last in a competitive market.
Key Takeaways:
- Importance of Quality Control: Quality control is essential in supplement manufacturing to ensure product safety, potency, and compliance with industry standards, protecting both consumers and manufacturers' reputations.
- Safety and Effectiveness: Stringent testing, such as raw material testing, in-process monitoring, and final analysis, is critical for guaranteeing the safety of supplements and ensuring they deliver the promised health benefits.
- Adherence to Industry Standards: Supplement manufacturers must comply with Good Manufacturing Practices (GMP), FDA regulations, and safety protocols like contaminant screening and active ingredient verification to ensure consistency and consumer trust.
- Future Trends: Innovations in testing technology, such as high-performance liquid chromatography (HPLC) and mass spectrometry, and global harmonization of standards are transforming quality control processes, ensuring faster, more reliable manufacturing and enhancing global consumer trust.
Explore the Critical Role of Quality Control in Supplement Production
Quality control in supplement production serves as a fundamental pillar that ensures products align with stringent standards. It runs through every stage of manufacturing, checking that each batch is consistent and accurate. That work is what keeps customers safe and willing to trust health and wellness products.
Safety of Consumers
Quality control in supplement production plays a vital role in ensuring consumer safety. It involves rigorous testing at various stages to prevent contamination and guarantee that only safe ingredients reach the shelves. By implementing strict quality measures, companies help avoid health risks associated with impurities and ensure that supplements are consumed with confidence. Customers rely on these checks every day, often without knowing it, which is why thorough quality control matters.
Meeting Industry Standards
Meeting industry standards is what keeps products sound and customers confident. These standards, set by the FDA through its current Good Manufacturing Practice (cGMP) rules, ensure that products are manufactured in a controlled environment with rigorous oversight and quality control. Compliance with these guidelines means that supplements not only meet the required safety criteria but also adhere to labeling and dosage accuracy protocols. This stringent adherence helps maintain consistency and quality across all batches, providing consumers with peace of mind.
Ensuring Product Effectiveness
Ensuring product effectiveness is a core aspect of quality control in supplement production. This process verifies that supplements deliver the health benefits they promise by maintaining the correct potency of active ingredients throughout the production and shelf life. Rigorous testing procedures ensure the efficacy of formulations, guaranteeing that each dose delivers the intended nutritional values and benefits. By doing so, manufacturers build credibility and trust with consumers who expect reliable and effective results from their supplements.
Essential Quality Control Steps in Supplement Manufacturing
As the supplement industry grows, manufacturers must adhere to rigorous processes to ensure product consistency and uphold stringent safety standards. Quality control is the checkpoint at every step of the production line. This dynamic process involves continuous assessment and refinement of methodologies to maintain the utmost integrity and potency in every supplement batch.
Testing Raw Materials
Testing raw materials is a foundational step in supplement manufacturing that ensures the purity, quality, and safety of the final product. Before any production begins, raw materials undergo a series of stringent tests to verify their identity, potency, and absence of contaminants. Careful checks like these prevent adulteration or contamination that could make a supplement less effective or unsafe. By prioritizing high-quality ingredients from reputable sources, manufacturers can produce superior products that meet and exceed consumer expectations.
In-Process Monitoring
In-process monitoring confirms that supplements meet quality standards while they are being manufactured. This continuous observation and testing throughout the production cycle prevent deviations from the set formulations and processes. By catching inconsistencies early, manufacturers can address issues before they impact the final product, guaranteeing uniformity and preventing recalls. Such monitoring involves real-time checks of equipment operation, batch consistency, and environmental controls, thereby safeguarding product integrity at every stage.
Final Analysis
The final analysis is the concluding checkpoint in supplement production, guaranteeing that the product meets all quality and safety criteria before it reaches consumers. This thorough assessment includes verifying the potency, purity, and overall composition of the supplement formula. A full evaluation confirms that the finished product is free from contaminants and matches the label. This step provides an additional layer of certainty, reinforcing consumer trust in the brand's commitment to quality.
Ingredients Safety Standards Required for Supplements
Ensuring consumer protection and upholding product integrity are central to the oversight of dietary supplements. The rules require complete labeling and a pre-market notification for new dietary ingredients. Such measures prioritize transparency, detailing ingredient specifics and safety parameters to mitigate risks associated with concentrated ingredient consumption.
Contaminant Screening
Contaminant screening is a critical safety standard in dietary supplement manufacturing designed to identify and eliminate unwanted substances that could compromise product safety and efficacy. This process involves testing for heavy metals, microbial contamination, pesticides, and other harmful substances, including unwanted mineral contaminants, that could affect consumer health. Ensuring that supplements are free from these contaminants helps maintain their purity and quality. By implementing thorough screening techniques, manufacturers protect consumers and uphold their brand's reputation for delivering safe and reliable products.
Active Ingredients Verification
Active ingredient verification confirms that a supplement contains the amounts stated on the label, for example of vitamin C or calcium. This verification process includes advanced analytical techniques to ensure these dietary supplement ingredients, such as vitamin C, are present in their proper potency and form. Accurate verification not only provides product effectiveness but also prevents misleading labeling. By prioritizing this critical step, manufacturers build trust with consumers, who can feel assured that they are getting the health benefits they expect from each dietary supplement, including vitamin E and calcium supplements.
Good Manufacturing Practices for Quality Assurance
Good Manufacturing Practices (GMP) for Quality Assurance emphasizes the establishment of detailed written procedures, ensuring that products consistently meet their specifications, and adhering to rigorous principles for sanitation and contamination prevention. It requires full record-keeping and proper handling of rejected products, so quality and safety standards hold throughout manufacturing.
Supplement Production GMP
Supplement Production under Good Manufacturing Practices (GMP) is essential for maintaining quality and consistency in the industry. These practices set rules for everything from keeping facilities clean to running strict process controls. By adhering to Good Manufacturing Practice (GMP) standards, manufacturers ensure that products are produced in a systematic and controlled manner, thereby minimizing the risk of errors or contamination. This framework supports the production of high-quality dietary supplement products that reliably meet consumer expectations.
Role of QA Teams
Quality Assurance (QA) teams oversee the whole production process to make sure quality standards are met. They are responsible for implementing and maintaining stringent quality checks at every stage, from sourcing raw materials to final product testing. QA teams ensure compliance with regulatory requirements, manage audits and address any quality-related issues promptly. Their careful work means customers get safe, effective supplements, and it strengthens the manufacturer's reputation for reliability.
Future Trends in Supplement Quality Assurance
Quality assurance matters especially for supplements, because the FDA does not approve them before they are sold. Stakeholders are increasingly turning to third-party verification systems to uphold rigorous standards for supplements. Ensuring strict adherence to dietary supplement regulatory requirements and independent oversight helps maintain consumer trust and market integrity.
Innovations in Testing Technology
Innovations in testing technology are transforming dietary supplement quality assurance by enhancing accuracy and efficiency. Advanced methods, such as high-performance liquid chromatography (HPLC) and mass spectrometry, enable the precise analysis of complex formulations, ensuring the accurate quantification of active ingredients. Additionally, the development of rapid testing kits enables quicker detection of contaminants and adulterants, reducing the time between production and market delivery. These technological advancements not only enhance consumer safety but also speed up the manufacturing process, enabling manufacturers to maintain high standards more effectively.
Global Harmonization of Standards
Global harmonization of standards is becoming increasingly important in the supplement industry, offering a unified approach to quality and safety protocols across different markets. This alignment involves standardizing testing methods, manufacturing practices, and regulatory requirements internationally, facilitating smoother cross-border trade and ensuring consistent quality. For consumers, global standards offer reassurance that their supplements meet stringent criteria, regardless of where they are produced. For dietary supplement manufacturers, it simplifies compliance and improves market access, building broader acceptance and trust.
Final Thoughts
Supplement quality control is indispensable in ensuring consumer safety, product effectiveness, and compliance with industry standards. Through rigorous steps, including raw material testing, in-process monitoring, and final analysis, manufacturers can produce high-quality products that meet regulatory requirements. Careful QA work and GMP compliance add further protection, so customers get safe and reliable supplements. The result is lasting trust and credibility with customers, and a healthier industry overall.
FAQs
How does quality control improve supplement safety?
Quality control enhances supplement safety by ensuring products are free from contaminants, accurately labeled, and manufactured under controlled conditions. It involves rigorous testing at each production stage, from raw materials to final products, to detect and address any potential issues that may arise. This systematic approach prevents the presence of harmful impurities and ensures that consumers receive safe, reliable supplements.
What certifications should consumers look for in supplements?
Consumers in the United States should look for certifications such as GMP, NSF International, and USP Verified when selecting food supplements. These certifications indicate that the product has met high standards for quality, safety, and label accuracy through rigorous testing and validation processes. They provide reassurance that the supplements are produced under strict quality controls.
How can I report a problem with a dietary supplement?
You can report a problem with a dietary supplement product or its manufacturer to the FDA through their Safety Reporting Portal. Provide details about the issue, including the product name, adverse effects, and any other relevant information. This enables regulatory bodies to take action and enhance consumer safety standards.
// Our Services
What Do You Need?
Select the service that matches your need. Each card expands to show what's included, minimum orders, and certifications then routes you directly to the right section of the form below.
F.A.M.E. Health Labs
Contract Manufacturing
Full-service supplement manufacturing from stock to custom white label, private label, co-manufacturing, and bulk.
See Services



F.A.M.E. Ingredients
Ingredient Sourcing
Global raw material sourcing, proprietary blend development, MOSA Organic, Halal and Kosher flavor systems.
See Services
Curí Inc.
Testing & CRO
ISO/IEC 17025 accredited testing ingredient and finished product. COAs accepted globally by FDA, Health Canada, and EU.
See Services

F.A.M.E. Complete
Enterprise Partnership
Full-platform commercial partnership for high-volume brands. Dedicated team, VP-level account management, real-time portal.
See Services