// Blog post
BCAA Manufacturing Process: Achieving Excellence from Science to Shelf
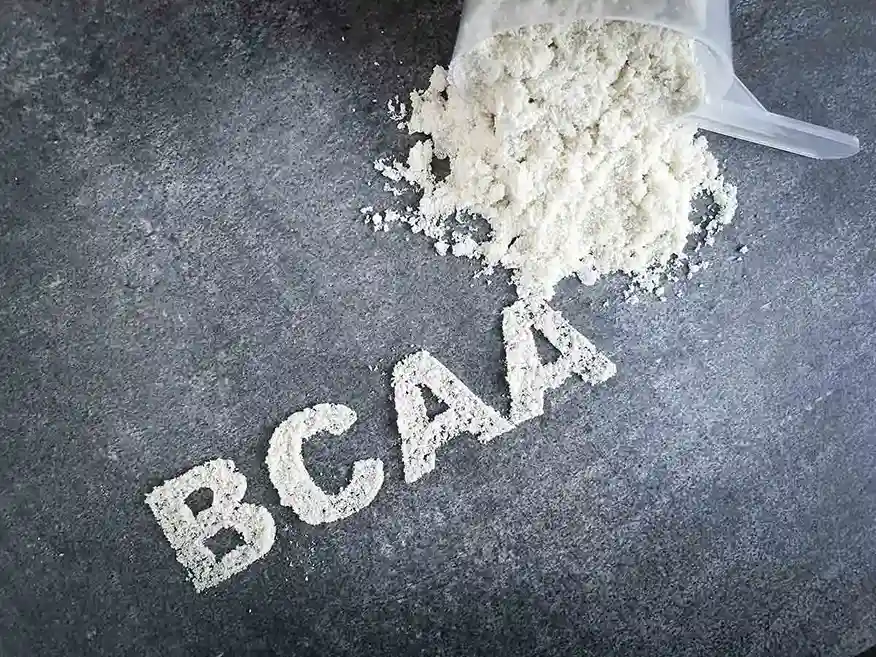
Table of Contents




Recent Posts
Popular posts
Certifications


Branched-chain amino acids (BCAAs) leucine, isoleucine, and valine are essential for muscle growth, recovery, and overall performance. These amino acids support protein synthesis and help reduce exercise fatigue.
At F.A.M.E. Health Labs, we ensure every BCAA product meets the highest standards through advanced manufacturing techniques and strict regulatory compliance. Explore how our end-to-end process turns science into shelf-ready quality.
Planning a BCAA product of your own? See how we handle powder manufacturing: blending, flavor work and testing on one Georgia campus, with white label from 500 units.
Key Takeaways
- Advanced Manufacturing Capabilities: F.A.M.E. Health Labs manufactures high-quality, science-backed supplements.
- Versatile Product Development: Beyond BCAAs, we manufacture a wide range of supplements, including probiotics and women's health products, tailored to each brand’s goals.
- Market-Ready Solutions: We turn complex formulations into shelf-ready products and handle each step from concept to commercialization.
Why Quality Begins with the Right Process
Quality in BCAA supplements starts with choosing the correct manufacturing process tailored to meet rigorous industry standards. This involves selecting appropriate raw materials and reliable production methods while ensuring compliance with health and safety guidelines. Every step from sourcing ingredients to packaging affects the end product’s efficacy and consumer trust.
At F.A.M.E. Health Labs, our approach to quality combines advanced technology with strict oversight at every stage of production. We focus on maintaining potency, purity, and performance across all BCAA formulations. Our processes are designed not only to meet but to exceed regulatory and consumer expectations, ensuring every supplement delivers consistent, science-backed results.
What Are the Main BCAA Production Methods
There are several primary BCAA production steps and formulation processes, each offering distinct advantages depending on production scale, dietary requirements, and brand goals. Understanding how BCAAs are manufactured forms the foundation of any effective BCAA manufacturing guide.
| Production Method | Process Overview | Key Advantages | Considerations |
|---|---|---|---|
| Microbial Fermentation | Uses selected microorganisms to naturally synthesize amino acids, ensuring high purity and bioavailability. |
|
|
| Chemical Synthesis | Chemical reactions convert raw materials into amino acids for rapid, large-scale production. |
|
|
| Enzymatic Hydrolysis | Enzymes break down proteins into BCAAs for better absorption. |
|
|
From Raw BCAA to Shelf‑Ready Product
Once the BCAAs are produced, the next stage of the BCAA manufacturing steps focuses on transforming the raw materials into consumer-ready formats. This section breaks down each phase.
Granulation Techniques
Granulation techniques transform raw BCAA powder into uniform granules, enhancing flowability and mixing for consistent dosage in supplements. This process improves the handling and compaction properties of the ingredients, vital for tablet formations. Granulation prevents ingredient separation, ensuring uniformity in each serving, and reduces the risk of dust formation, critical for maintaining product quality and safety during manufacturing and consumption.
Blending & Flavoring
Blending and flavoring involve mixing BCAAs with other ingredients and enhancing the taste to create a palatable product. Proper blending ensures uniform distribution of nutrients, while carefully chosen flavoring agents enhance consumer appeal without compromising nutritional value. This step decides whether the product tastes good enough for customers to take it every day. These improvements help ensure that BCAAs can be both functional and flavorful.
Final Drying & Packaging
Final drying reduces moisture in BCAA products, ensuring stability and shelf life, while packaging provides protection from environmental factors. This step ensures consistency, preventing clumping and degradation. High-quality materials are used for packaging to maintain freshness and comply with safety standards. This careful attention to drying and packaging solutions safeguards product integrity until it reaches consumers, reflecting a commitment to delivering superior supplements.
Functional Excipients That Enhance Formulations
Excipients play a significant role in product performance and user experience. Learn how binders, coatings, and stability agents impact the final quality of BCAA supplements.
Binders
Binders are essential in the formulation process, providing cohesion to BCAA supplements, especially tablets, ensuring they hold together effectively. They contribute to the structural integrity and ease of handling, delivering precise dosages. Choosing the right type influences disintegration rates and bioavailability, enhancing the supplement's effectiveness while ensuring a consistent and user-friendly product.
Coatings
Coatings protect BCAA supplements, improving stability and extending shelf life. They improve the taste and mask any unpleasant odors, ensuring a more enjoyable consumption experience. Additionally, coatings can provide specific release profiles, like slow or sustained release, aligning with various health and wellness goals while safeguarding the supplement's efficacy.
Stability Agents
Stability agents keep BCAA supplements effective over time. They prevent degradation caused by environmental factors such as heat, light, and moisture. By ensuring the product remains potent and effective until consumption, stability agents contribute to the reliable performance of BCAAs. This helps maintain consumer trust and ensures a quality experience in every dose.
Experience End-to-End Innovation and Compliance in the BCAA Manufacturing Process with F.A.M.E. Health Labs
Partnering with an experienced BCAA supplement manufacturer like F.A.M.E. Health Labs ensures consistency, compliance, and superior product performance. Based in the USA, F.A.M.E. Health Labs is an FDA-registered manufacturer holding cGMP, NSF, and SQF certifications, reflecting our commitment to the highest safety and quality standards. Our campus in Cedartown, Georgia covers every step, from ingredient sourcing to the finished product. Each BCAA batch is checked against strict benchmarks for purity and consistency, with testing by CURI, our ISO 17025 sister lab on the same campus. We support brands with custom supplement formulations, regulatory compliance strategies, and go-to-market execution. For BCAAs, probiotics, or products in the women’s health category, our science-backed processes and full-spectrum support turn complex ideas into high-demand, shelf-ready products tailored to your brand’s vision.
Final Thoughts
High-quality BCAA manufacturing involves a combination of science, precision, and a commitment to excellence. From raw material selection to final packaging, every step impacts the supplement’s quality, safety, and effectiveness.
By applying the right BCAA manufacturing steps and technologies, brands can confidently offer products that meet evolving consumer expectations. F.A.M.E. Health Labs provides full-spectrum manufacturing solutions in the USA. We help brands improve a current product or launch a new one.
FAQs
How is BCAA purity verified during large‑scale manufacturing?
BCAA purity is verified through rigorous testing methods, including high-performance liquid chromatography (HPLC) and mass spectrometry. These techniques ensure accurate measurement of amino acid concentration and detect impurities, guaranteeing that each batch meets strict quality standards throughout large-scale production.
Which factors most impact the yield in microbial fermentation of BCAAs?
The yield in microbial fermentation of BCAAs is primarily influenced by the strain of microorganism used, nutrient availability, pH levels, temperature, and fermentation time. Optimizing these factors accelerates microbial growth and enhances amino acid production efficiency, resulting in higher yields.
What steps ensure batch‑to‑batch consistency in BCAA powder production?
Batch-to-batch consistency in BCAA powder production is ensured through standardized operating procedures, precise ingredient measurements, and real-time monitoring. Regular quality checks and calibration of equipment further maintain uniformity, minimizing variations and ensuring each production cycle meets established quality and efficacy standards.
How are BCAAs manufactured to meet vegan and allergen‑free claims?
BCAAs are manufactured to meet vegan and allergen-free claims by using plant-based raw materials and microbial fermentation processes. This approach eliminates animal-derived ingredients and common allergens. Strict cross-contamination protocols and thorough facility cleaning further ensure that the final product aligns with these dietary requirements.
What U.S. regulations must a BCAA manufacturing facility comply with?
A BCAA manufacturing facility in the U.S. must register with the FDA as a food facility, follow the dietary supplement Current Good Manufacturing Practices rule (cGMP, 21 CFR Part 111), and meet FDA labeling rules for supplements under the Dietary Supplement Health and Education Act (DSHEA). These regulations ensure product safety, quality, and accurate labeling to protect consumer interests.
How is clumping and moisture absorption prevented in BCAA powders?
Clumping and moisture absorption in BCAA powders are prevented through the use of anti-caking agents and desiccant packets in packaging. Proper drying and airtight packaging also keep the product stable by limiting moisture exposure during storage and transportation.
// Our Services
What Do You Need?
Select the service that matches your need. Each card expands to show what's included, minimum orders, and certifications then routes you directly to the right section of the form below.
F.A.M.E. Health Labs
Contract Manufacturing
Full-service supplement manufacturing from stock to custom white label, private label, co-manufacturing, and bulk.
See Services




F.A.M.E. Ingredients
Ingredient Sourcing
Global raw material sourcing, proprietary blend development, MOSA Organic, Halal and Kosher flavor systems.
See Services
Curí Inc.
Testing & CRO
ISO/IEC 17025 accredited testing ingredient and finished product. COAs accepted globally by FDA, Health Canada, and EU.
See Services

F.A.M.E. Complete
Enterprise Partnership
Full-platform commercial partnership for high-volume brands. Dedicated team, VP-level account management, real-time portal.
See Services